 EN
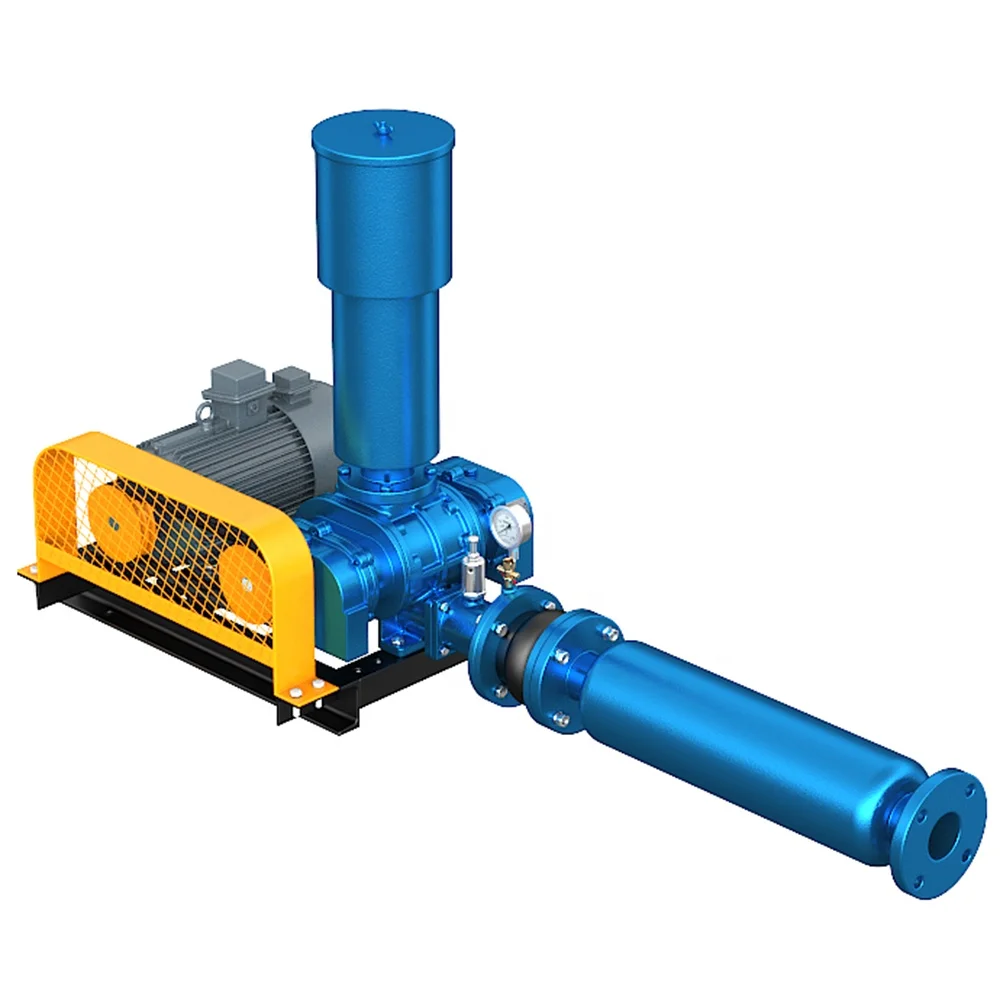
A lobe roots blower represents a critical investment for facilities managing positive displacement blower applications across manufacturing, wastewater treatment, pneumatic conveying, and environmental control sectors. These robust rotors operate under demanding conditions, making preventive maintenance essential for maximizing operational efficiency and extending equipment lifespan. Understanding proper care practices directly impacts your bottom line by reducing unplanned downtime, minimizing repair costs, and ensuring consistent performance in industrial air compression systems.
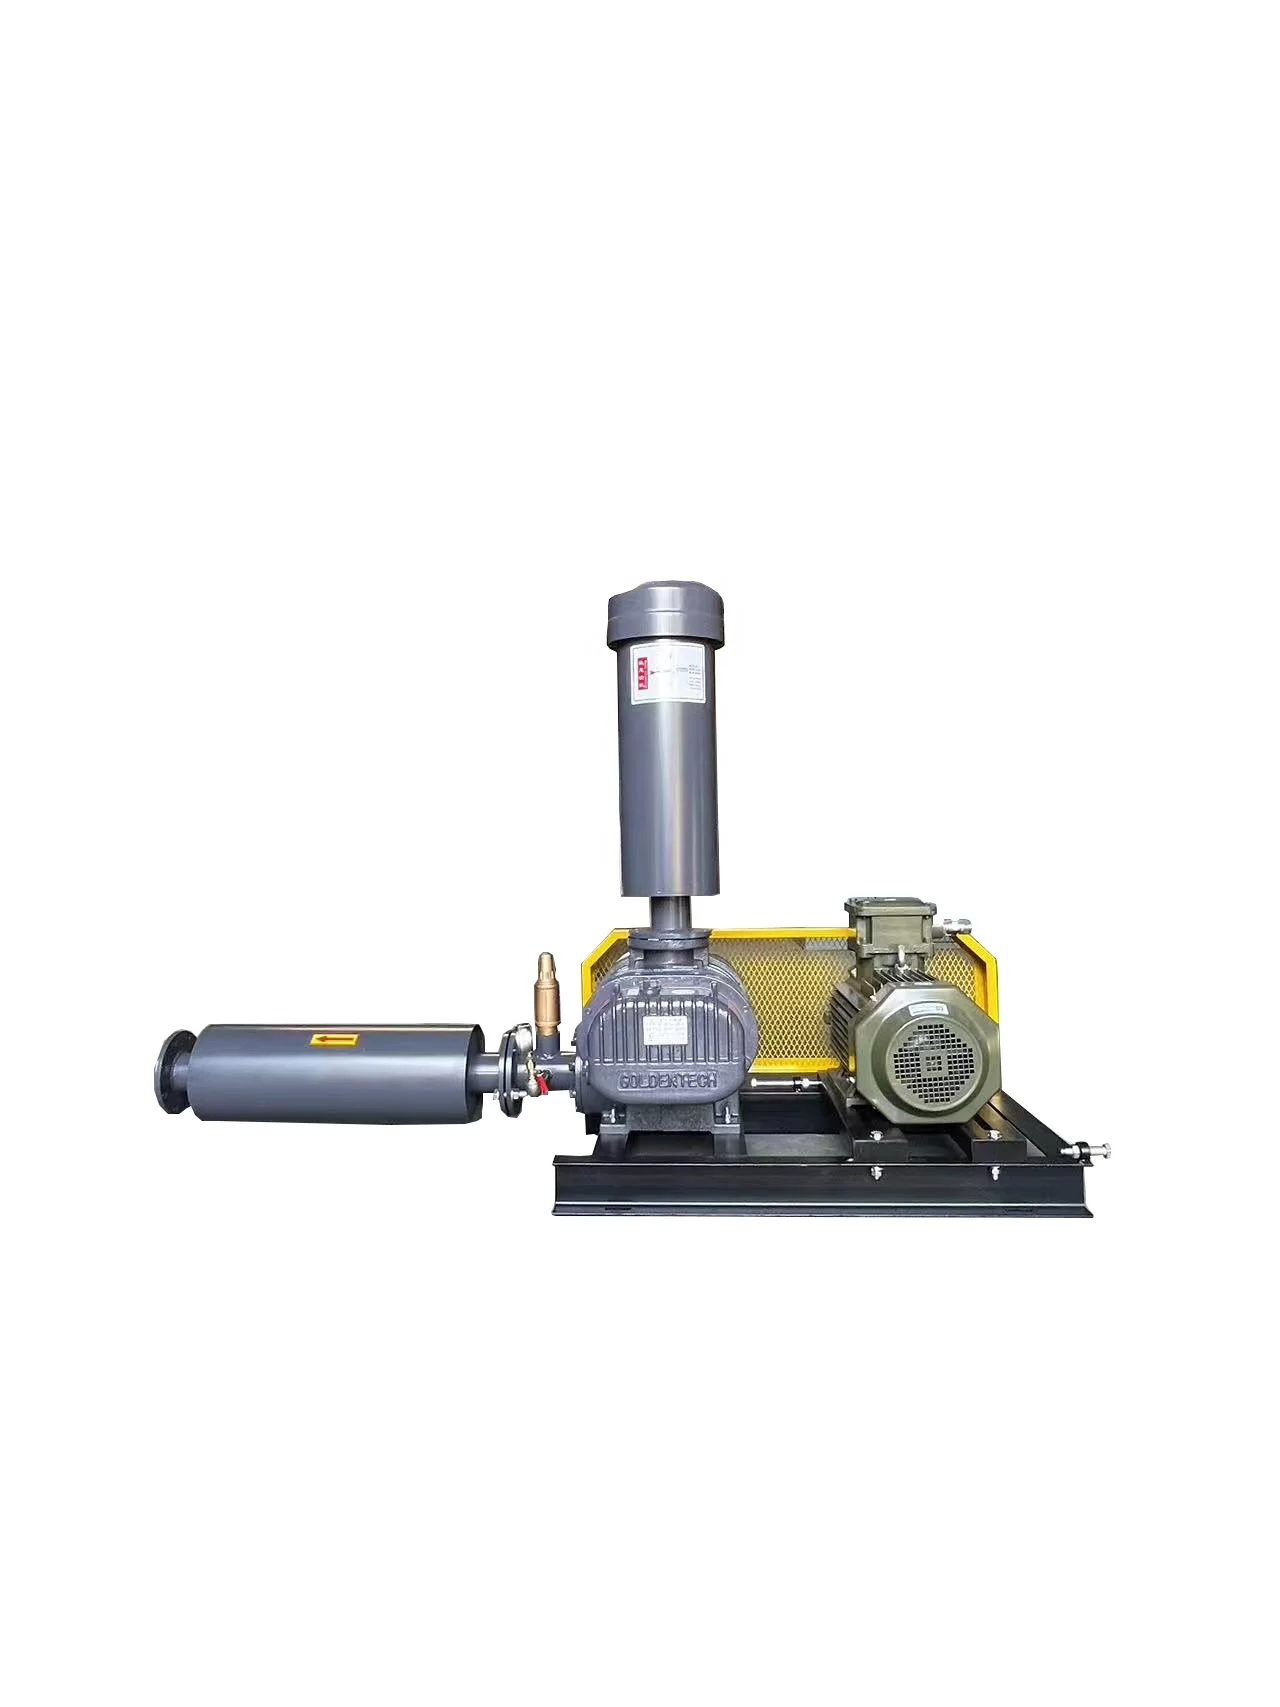
Rotary lobe blower maintenance and troubleshooting begins with recognizing that preventive action dramatically outperforms reactive repair. Industrial air compression systems depend on precise mechanical tolerances, clean operating environments, and consistent lubrication. By implementing systematic maintenance protocols tailored to your specific positive displacement blower applications, you protect your equipment investment and maintain reliable airflow when production demands it most.
Oil and Lubrication Management
Selecting the Right Lubricant Grade
Choosing appropriate oil is foundational to lobe roots blower longevity. The rotors spin at high speeds while maintaining minimal clearances, creating conditions where inadequate lubrication causes rapid bearing wear and seal degradation. Consult your equipment documentation for the manufacturer's recommended viscosity grade and synthetic versus mineral oil specifications. Most positive displacement blower applications benefit from synthetic oils that resist thermal breakdown and maintain stable viscosity across temperature fluctuations. This matters particularly in facilities where ambient conditions vary seasonally or where process heat influences operating temperature.
Oil Change Intervals and Monitoring
Establishing consistent oil change schedules prevents acid accumulation and particle buildup that degrade rotary lobe blower maintenance effectiveness. For typical industrial air compression systems, quarterly or biannual oil changes represent reasonable starting points, though your actual interval depends on operating hours, ambient contamination levels, and equipment age. Implement oil analysis testing to monitor viscosity degradation, particle contamination, and acid content between scheduled changes. This predictive approach transforms maintenance from a calendar-driven routine into a condition-responsive strategy that adapts to actual equipment wear patterns. Clean oil protects internal components while reducing friction losses that otherwise diminish overall efficiency.
Filtration and Air Quality Control
Intake Filter Maintenance
Contaminated inlet air accelerates wear on rotary components and compromises the integrity of rotary lobe blower maintenance efforts. Atmospheric dust, moisture, and particulates enter the blower housing and deposit on rotor surfaces, creating friction and heat generation that shortens bearing life. Install appropriate intake filters matched to your facility's environmental conditions and change them according to pressure differential monitoring rather than arbitrary schedules. Facilities near industrial areas or construction zones may require monthly filter changes, while cleaner environments support longer intervals. For positive displacement blower applications in sensitive environments, consider multi-stage filtration with water separation capabilities to address both particulate and moisture contamination.
Discharge Line Care
Downstream filtration protects external components and maintains system reliability. Discharge-side filter elements trap rotor wear debris, oil aerosol, and process contamination before air enters downstream equipment or customer processes. Regular inspection and timely replacement prevent backpressure buildup that forces rotors to work harder and generate excessive heat. This attention to industrial air compression systems cleanliness preserves positive displacement blower applications performance and extends equipment service intervals significantly.
Temperature Monitoring and Thermal Management
Detecting Overheating Conditions
Temperature elevation serves as an early warning indicator for potential lobe roots blower problems. Normal operating temperatures typically fall within 180–220 degrees Fahrenheit depending on design specifications and ambient conditions. Sustained temperatures above manufacturer recommendations signal bearing stress, internal friction, or inadequate cooling. Install temperature sensors at bearing housings and discharge outlets to create continuous monitoring data. When rotary lobe blower maintenance alerts indicate rising trends, investigate possible causes such as internal clearance changes, bearing degradation, or cooling system blockages before catastrophic failure occurs.
Cooling System Effectiveness
Most industrial air compression systems employ oil cooling or water-jacket cooling to dissipate operational heat. Verify that cooling passages remain clear of debris, scale buildup, or process contamination that restricts flow and reduces heat removal capacity. For water-cooled positive displacement blower applications, monitor inlet and outlet temperatures to calculate cooling effectiveness. Inspect coolant hoses for cracks or deterioration, as cooling system leaks compound thermal stress while creating secondary contamination risks. Maintaining thermal stability protects bearings from accelerated aging and preserves seal elasticity that prevents oil leakage and environmental contamination.
Seal and Bearing Inspection
Seal Condition Assessment
Oil seals prevent lubricant loss and protect bearing cavities from external contamination entering rotary lobe blower assemblies. Regular visual inspection identifies weeping, which indicates seal aging, or more concerning active leaking that requires immediate attention. Seal degradation accelerates when exposed to excessive heat, chemical attack, or mechanical stress from bearing deflection. For positive displacement blower applications operating continuously, plan seal replacement during scheduled maintenance windows rather than waiting for emergency failures. Proactive seal replacement costs far less than emergency downtime and secondary damage to bearing surfaces exposed by seal failure.
Bearing Wear Detection
Bearing condition directly determines lobe roots blower reliability and operational lifespan. Listen for unusual grinding noises, vibration changes, or temperature spikes concentrated at bearing locations. Elevated vibration levels suggest bearing radial play or surface degradation requiring replacement. Industrial air compression systems benefit from vibration analysis programs that establish baseline signatures and alert technicians when measurements deviate significantly. Early bearing replacement prevents catastrophic failure modes where collapsed bearings allow rotor contact, destroying the equipment and creating dangerous system pressurization. Rotary lobe blower maintenance programs incorporating bearing inspections typically extend equipment life by 30–50 percent compared to reactive repair approaches.
FAQ
How frequently should oil be changed in a lobe roots blower?
Most manufacturers recommend oil changes every 500–1000 operating hours or quarterly, whichever comes first. However, actual intervals depend on your specific positive displacement blower applications, ambient cleanliness, and operating temperature. Implementing oil analysis testing helps determine if your equipment can safely extend intervals or requires more frequent changes to maintain rotary lobe blower maintenance standards.
What signs indicate a lobe roots blower needs maintenance?
Rising discharge temperatures, increased vibration, unusual noise, oil leakage, or declining pressure output signal that rotary lobe blower maintenance and troubleshooting should begin immediately. These indicators suggest bearing wear, seal degradation, or internal clearance changes requiring professional inspection. Addressing these symptoms promptly prevents secondary damage and maintains reliability of industrial air compression systems supporting critical processes.
Can proper maintenance prevent lobe roots blower failure?
Systematic maintenance cannot eliminate all mechanical wear, but it dramatically reduces failure probability and extends overall equipment lifespan. Consistent oil changes, filter replacement, temperature monitoring, and bearing inspection create conditions where positive displacement blower applications operate reliably for 15–25 years. Well-maintained equipment rarely fails unexpectedly, allowing you to schedule replacements during planned maintenance windows rather than facing emergency shutdowns.